Lecture 32 min.
The arrival of 3D printers opened a new technological era – it is now possible to print a three-dimensional object. The purpose of the resulting three-dimensional products can be extremely varied – from toys to medical prostheses. The process is based on a digital model (or drawing), which is then realized as an exact physical copy of itself. Such machines come in various power ratings and configurations, in home and industrial versions. The types of 3D printers available today use a very wide range of materials to produce three-dimensional prints.
CONTENTS
The consumable loaded into the machine determines the types of 3D printers. Laser machines sinter and laminate powder. An inkjet 3D printer glues the layers of the source material together one after another, after which they are sintered. The next step is cooling. Various kinds of photopolymer plastic, resins, powders, silicone, metal and wax components can be used here. Let us look at how such machines work with different materials.
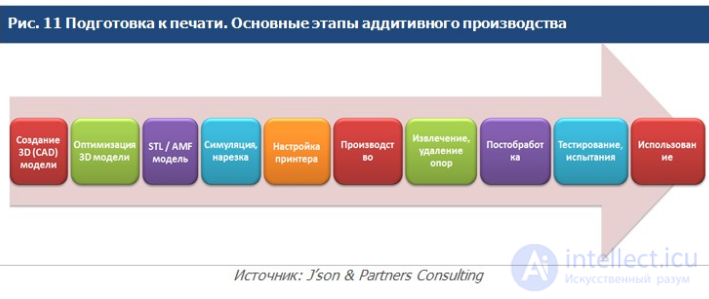
The operating principle of the machine consists of the following steps:
A device like this can quite realistically be built with your own hands – it is enough to have the necessary components. One more bonus "in the piggy bank" of such a machine is that it works with metal powder.
ABS plastic – acrylonitrile butadiene styrene – is a plastic whose name is made up of the initial letters of the substances whose polymerization produces it: acrylonitrile (A) with butadiene (B) and styrene (S). Or, to be more precise, butadiene and styrene-acrylonitrile copolymer (SAN).
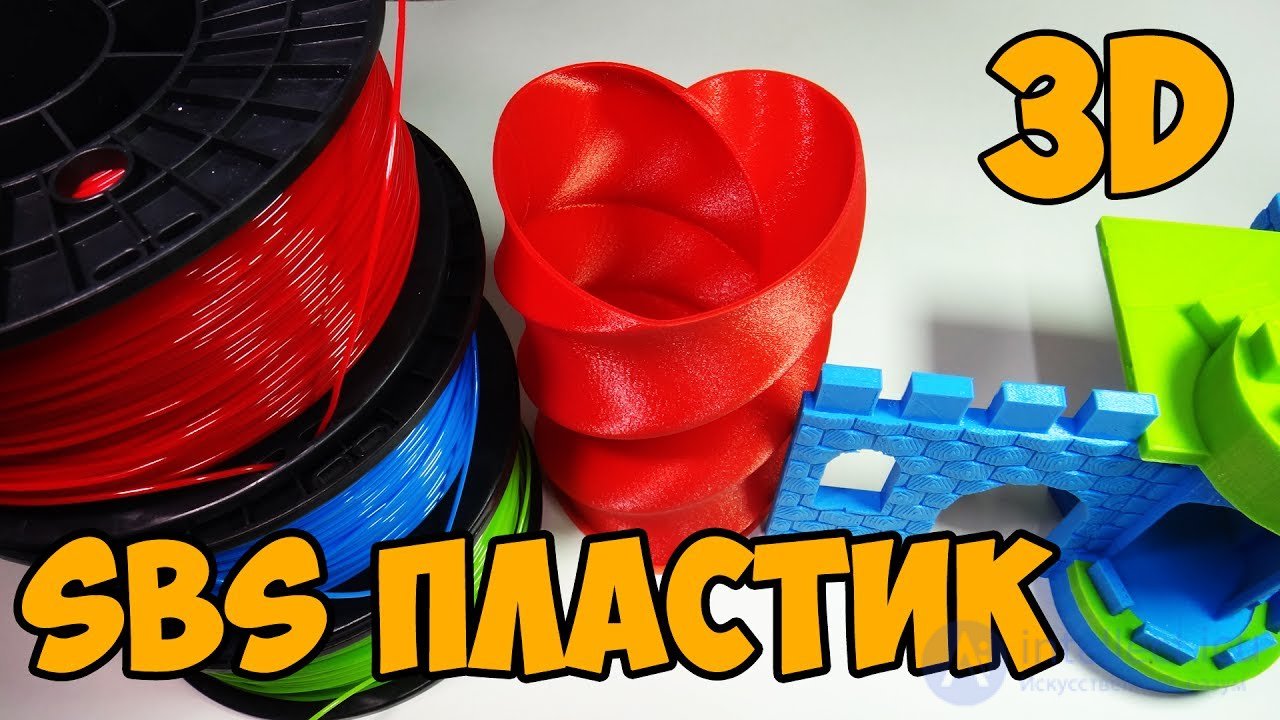
SBS. Strength, ductility and heat resistance make it a material that is often preferred in engineering and mechanical applications. Its modulus of elasticity is far lower than that of ABS. That is, the printed parts turn out more flexible. Elongation at break is >250%. Unlike ABS, the filament does not snap, let alone PLA, which is the most brittle of the materials under consideration. SBS has a flexible structure. It will not break off or tear during printing. Even if the filament is fed into your extruder at an angle of 90 degrees! The material is transparent (93% light transmission). Dyeing the material produces a very attractive effect. It can be processed and dissolved with limonene, dichloromethane and solvent naphtha. SBS is ideal for printing lamp shades, prototypes of transparent tableware, bottles and so on.
SBS is not afraid of open air or drafts. It sticks well to the bed. It can also be printed on an unheated bed. SBS Watson is well suited to printing large-scale models. Excellent interlayer adhesion (bonding between layers) adds extra strength to printed items. The plastic is approved for the manufacture of medical devices and children's toys.
SBS does not smell during printing. People with a very keen sense of smell may catch a faint odor (from some dyes) within 30 cm of the hot end, but no more than that. The transparent version has no odor at all.
SBS does not absorb moisture! It can simply be stored in a bag (to keep it from getting dusty). The filament does not become brittle from contact with moisture. Tableware can also be printed from it, and contact with cold foodstuffs is permitted.
SBS is a new and very promising material for 3D printing. In its properties it surpasses traditional ABS or PLA. If we give an overall assessment of the materials reviewed, SBS takes first place as a universal, undemanding, convenient and attractive material.
PETG for 3D printing
PETG. It is considered that PETG combines the advantages of ABS — strength, heat resistance, durability — with those of PLA — ease of printing. It is slightly more flexible than ABS and PLA, but stiffer than SBS. Layer fusion is generally excellent. Thermal shrinkage is low. There is far less reason to fear dimensional distortion in prints
PETG is likewise not afraid of open air or drafts. It sticks well to the bed. Heating the bed is not mandatory, but it can prove useful, especially if distortion of large parts is observed. It is entirely possible to print without heating, although you will have to fiddle with the settings a little. A very strong and durable material.
PETG has practically no smell, at least far less than ABS
PETG is practically unaffected by the ordinary humidity of the surrounding air, so no particular problems arise with printing and storage. Even so, it is good for the filament to be stored in as dry a place as possible, next to silica gel packets.
PETG is intended to replace ABS and PLA in the field of 3D printing; in its properties it surpasses these materials, and it is convenient to use, durable and safe.
PLA plastic
However, the main competitor of ABS plastic is PLA plastic, a biodegradable plastic – a so-called aliphatic polyester whose monomer is lactic acid. Such plastic is called biocompatible, since the main raw materials for its production are rapidly renewable resources, chiefly sugar cane and corn.
Manufacture of PLA plastic. materials for 3D printing, 3D printing with plastic, plastic for 3D printing, 3d printing, 3d-printing, materials for 3d-print, printer for 3d printing, three-dimensional printers, 3d prınter, 3 d printers, applications of a 3d printer, design of a 3d printer, capabilities of 3dPLA plastic. materials for 3D printing, 3D printing with plastic, plastic for 3D printing, 3d printing, 3d-printing, materials for 3d-print, printer for 3d printing, three-dimensional printers, 3d prınter, 3 d printers, applications of a 3d printer, design of a 3d printer, capabilities of 3d
In addition, biodegradable plastics are sometimes made from renewable raw materials such as starch (potato, corn, tapioca (a starchy grain from the root tubers of cassava) and so on), soy protein, cellulose and a few others. Ones that are not hazardous or toxic in production and that, after use, break down into carbon dioxide and water or into ecologically safe biomass (when composted).
So, the main advantage of PLA plastic is that it is non-toxic, and therefore it can safely be used to make toys and other items that pose no direct threat to human health – food-grade plastic, disposable tableware and the like.
PLA plastic has a lower filament softening temperature than ABS plastic (about 190°C), and a printing temperature of 210 to 250°C, which means working with it consumes less energy. On top of that, 3D printing with this plastic does not require Kapton (for coating the surface on which the prototype is built up). Nor is it necessary to heat the bed to "unstick" the object built up on it.
Items made of PLA plastic. materials for 3D printing, 3D printing with plastic, plastic for 3D printing, 3d printing, 3d-printing, materials for 3d-print, printer for 3d printing, three-dimensional printers, 3d prınter, 3 d printers, applications of a 3d printer, design of a 3d printer, capabilities of 3d
Another plus is the fairly smooth surface of an item printed from PLA plastic, good detail, and easy finishing by sanding or other methods that require no special equipment.
Among the drawbacks of PLA plastic for 3D printers is that it is somewhat more expensive than ABS plastic. And that it loses its original quality fairly quickly (compared with long-lasting ABS), and is therefore suitable only for making objects with a limited service life. The decomposition period of PLA plastic ranges from several weeks to several years, depending on the grade.
It can arguably be counted a drawback of PLA plastic that, unlike ABS plastic, it does not dissolve in acetone. On the other hand, PLA plastic is readily soluble in phenol, in concentrated sulfuric acid and in a substance called "limonene".
PVA plastic for 3D printing
In fairness it should be noted that a new kind of material for 3D printing has recently appeared on the market – PVA plastic (polyvinyl acetate). In fact it is the PVA glue familiar to everyone from school craft lessons, except that in this case PVA is diluted with water from a dry state to a certain consistency. And then, using special equipment, it is melted and formed into special pellets or PVA filament for 3D printing. It is still too early to speak about this kind of plastic and its particular advantages over other materials for 3D printing. It appeared on the market only in 2012.
PVA plastic. materials for 3D printing, 3D printing with plastic, plastic for 3D printing, 3d printing, 3d-printing, materials for 3d-print, printer for 3d printing, three-dimensional printers, 3d prınter, 3 d printers, applications of a 3d printer, design of a 3d printer, capabilities of 3d
PVA plastic is known to be used as a separator for printed parts, thanks to the fact that it dissolves readily in water. Here is an example: we print a part on a 3D printer, a nut screwed onto a bolt, using PVA plastic and some other plastic (ABS or PLA). And after printing we lower the finished prototype into water for a short time, after which we easily remove the nut. In this way, with the help of PVA plastic, we obtain several finished items in a single print run!
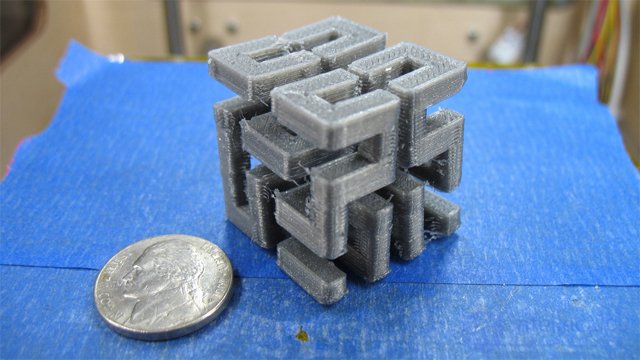
One of the main downsides of this material is its high price and its solubility in water – in some cases this is useful, and in others completely unacceptable. PVA plastic is worked at a temperature of 190°C, its melting point is 160–170°C, and its solidification (glass transition) temperature is 45–55°C.
Nylon for 3D printing
An even newer material for 3D printing is considered to be nylon. The material is highly resistant to a wide range of solvents and chemicals. Nylon from the company Taulman 3D is especially popular today.
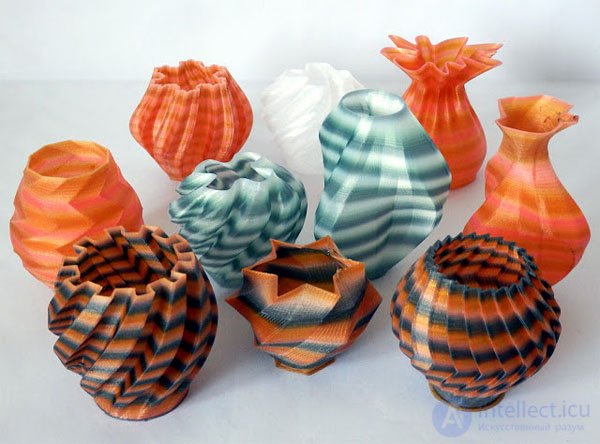
The gypsum variant is also loaded with powders, but with the appropriate ones – from gypsum to filler, cement and the like. A binding agent . Such printers are most often used to create interior decorations. The items produced here are extremely varied.
In this case, liquid photopolymers are used to make the objects. The principle behind creating figurines is interesting. Guided by the computer model, an ultraviolet laser exposes specific spots. These then harden under the action of the ultraviolet light. Such exposure can also be carried out through a specially prepared photomask – only in that case an ultraviolet lamp is used. The mask blank is changed with every new layer.
If stereolithographic equipment is chosen, you can enjoy very high precision in three-dimensional printing. The only drawback is the low operating speed, but when precision is what matters, the time taken is ignored.
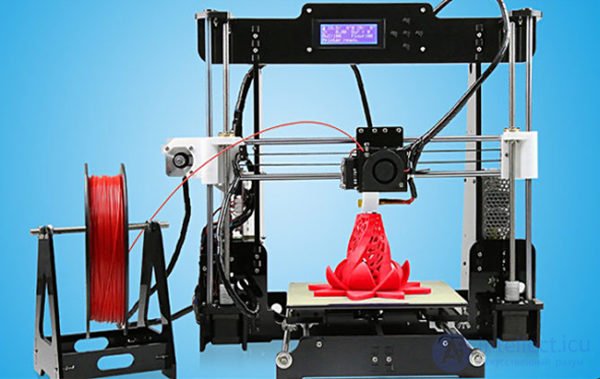
A machine of this kind prints using wax – a material with a low melting temperature. That property brings a bonus: it is easy to work with. This is why the sharpness and accuracy of the resulting contours are impeccable.
To produce objects in a wide range of colors, the machine uses a special head. It contains several extruders at once – components able to melt and deposit the consumable material being used.
For the most part, such units are employed in making children's toys. Another purpose is creating designer jewelry.
There is one more method, called "dye sublimation". This type of printer is used when an image (from a photograph, for example) has to be transferred onto a textured surface. To do this, the dyes are heated at specific spots – the heat makes them evaporate, and the required image remains.
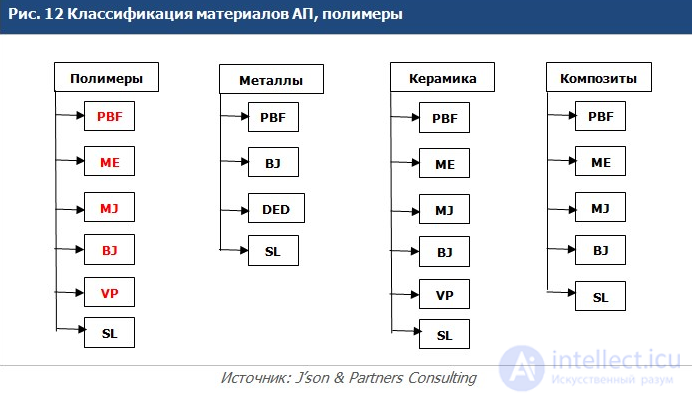
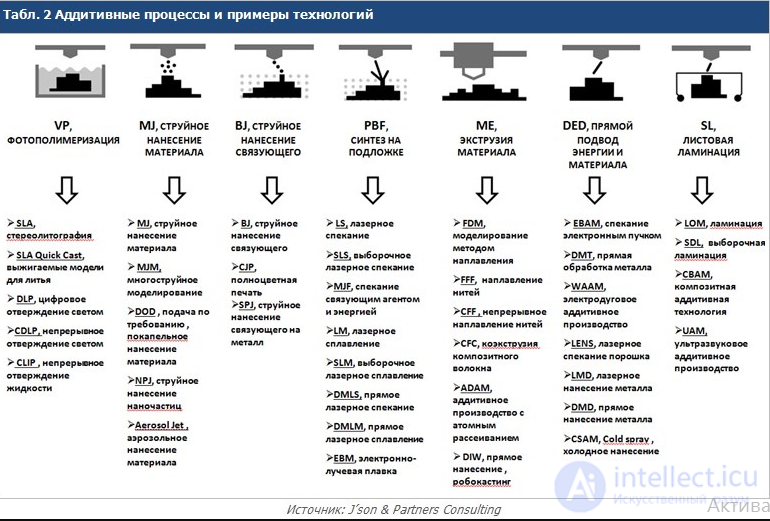
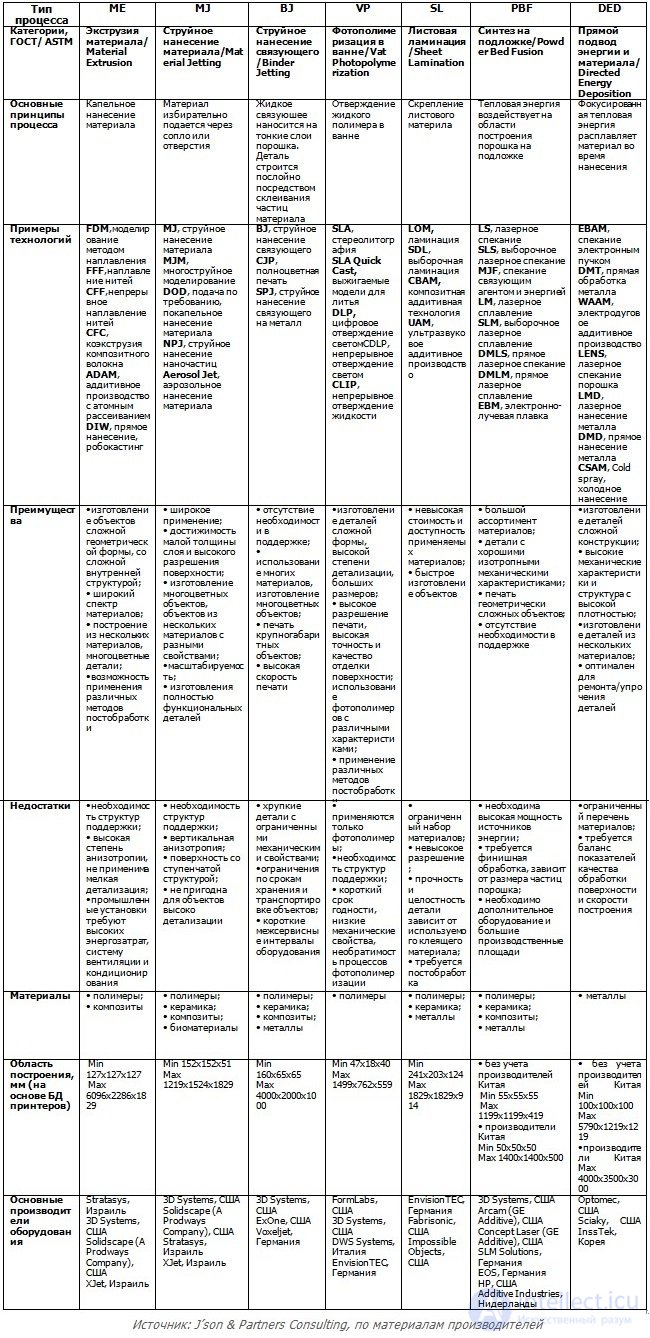
A special classification is applied to the technologies used, and it is worth knowing for every future owner of a 3D printer:
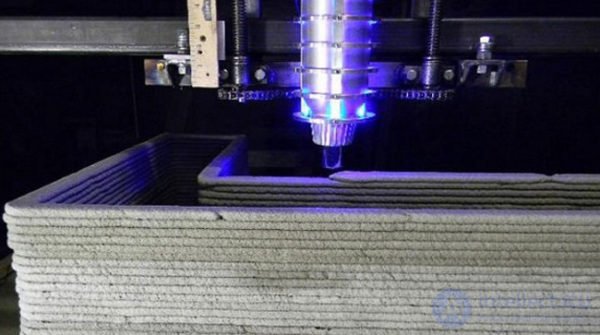
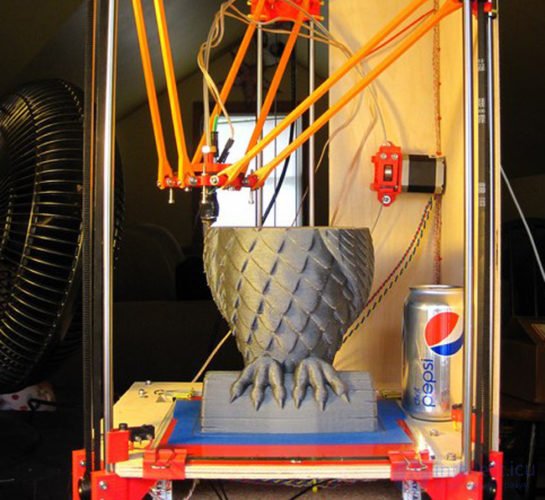
This is the most popular technology in the devices under consideration. With FDM (fused deposition modeling) the machine extrudes the consumable material through a special nozzle layer by layer. This group includes:
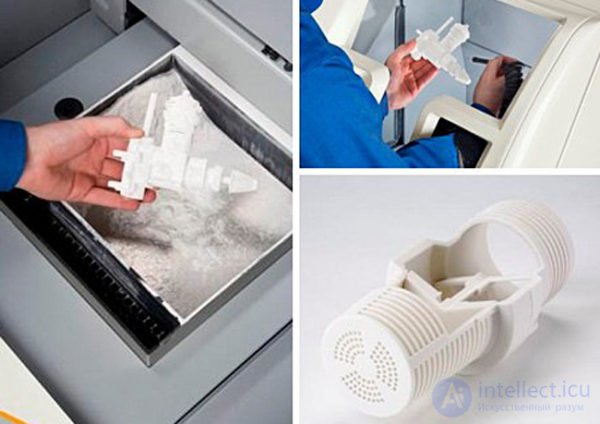
MJM (Multi Jet Modeling) is also of interest; it involves the technique of multi-jet modeling. The process resembles ordinary inkjet printing, since the material is fed through small nozzles (there can be several hundred of them). The specified three-dimensional model is built up as each previous layer sets.
The consumables are photopolymers and plastic; a special wax is also suitable. This kind of three-dimensional printing is usually used to make medical implants, dental prostheses and casts.
Multicolor versions are achievable, as are objects with differing properties – for example, flexible parts combined with rigid ones.
This technology also has drawbacks – very expensive raw material and a fragile result. It is usually applied in medicine and industrial prototyping.
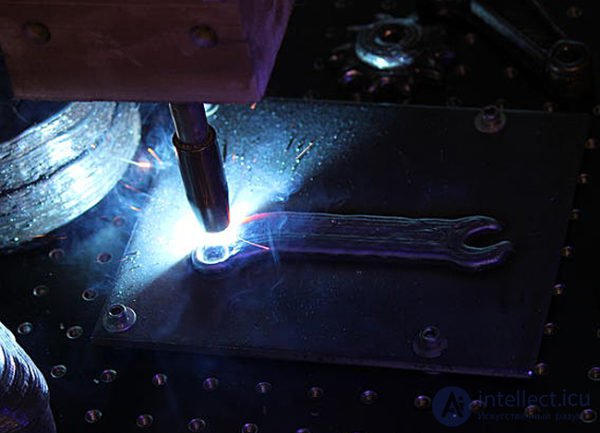
With LASER ENGINEERED NET SHAPING, the consumable material blown out of the nozzle immediately enters the focus of the laser beam, which brings about instant sintering. The use of metal powder made it possible to produce objects from steel and titanium, which opened the way to using 3D printers in industry. Many alloys can be mixed and obtained directly during the process. This is how titanium turbine blades are made, for instance.
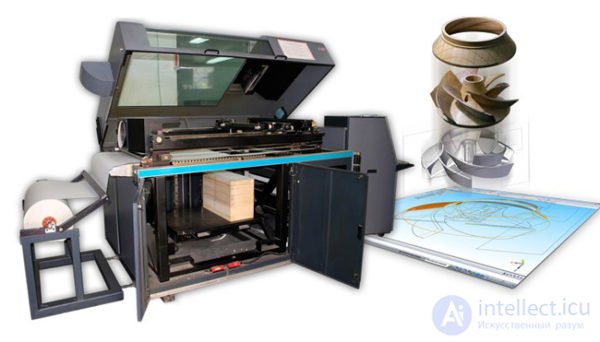
With Laminated Object Manufacturing, thin, already laminated sheets are cut by a laser and then glued, sintered or pressed together into a three-dimensional object. Plastic, aluminum and paper 3D objects can be printed this way.
Incidentally, the raw material for aluminum objects is the corresponding foil – it is "sintered" using ultrasonic vibration.
Despite the lightness of the raw material, paper models come out very strong, and their cost is next to nothing. But be prepared for the fact that such an item comes with a large amount of waste. Even that can be avoided, though, by arranging several small objects on a single sheet.
To understand how Stereolithography works, picture a vat filled with liquid polymer. A laser beam passing across its surface polymerizes a layer. Once one of the layers is finished, the platform lowers the part so that liquid polymer fills the voids. Then the arrangement is reversed: the part is raised upward, while the laser itself sits below.
This method requires surface finishing to sand down and remove excess material. Sometimes the result is additionally cured in ultraviolet ovens.
A printer of this kind should not be kept at home:
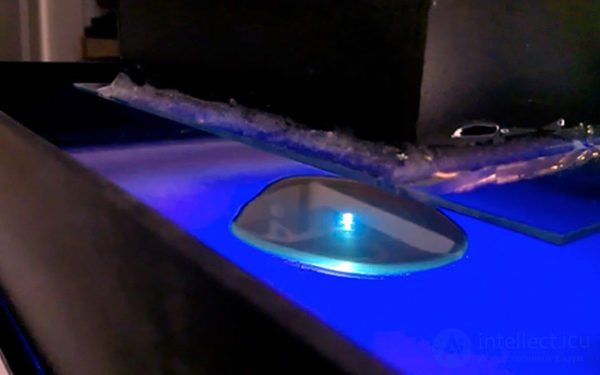
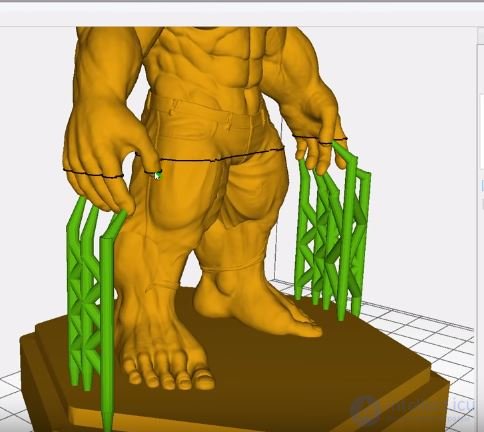
This technology resembles the type described above, but here a laser-fused powder is used instead of a photopolymer. There is no need to fear that the part will break during the process, and steel, nylon, bronze, titanium, ceramics, glass, casting wax and other materials can quite likely be used as the consumable.
The technology allows complex items to be created. It is excellent, for example, for making prototypes – for jewelry, say. The unfused powder serves as support for overhanging elements, which means there is no need to form any special support structures.
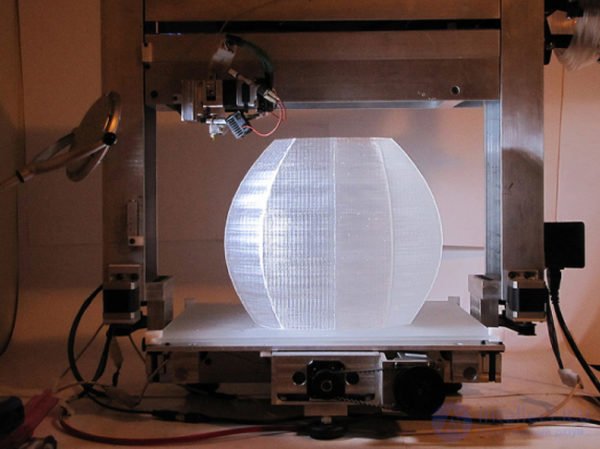
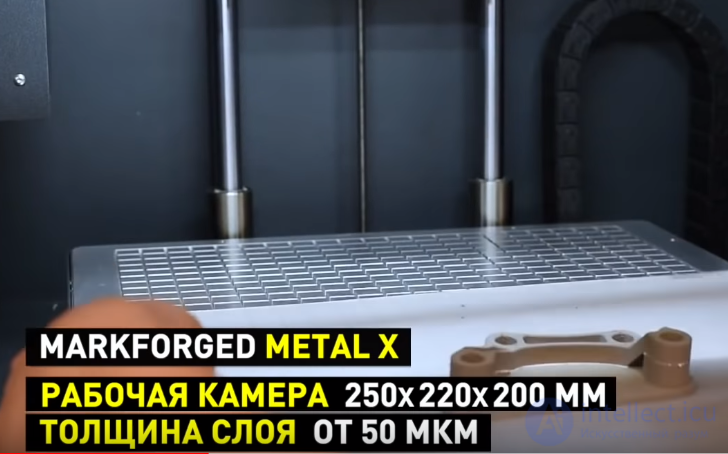
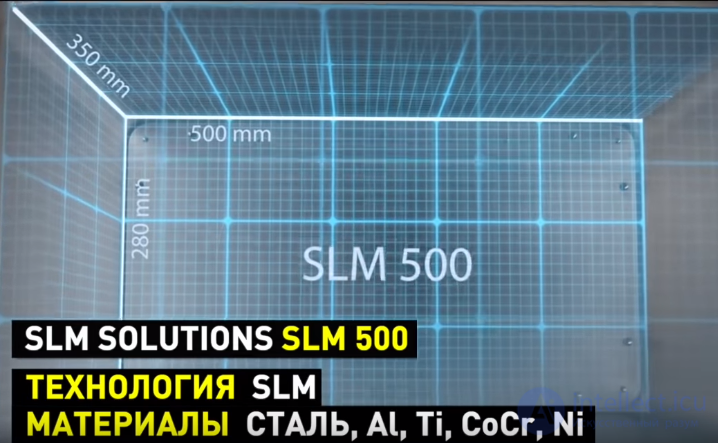
Ready-made metal printing systems
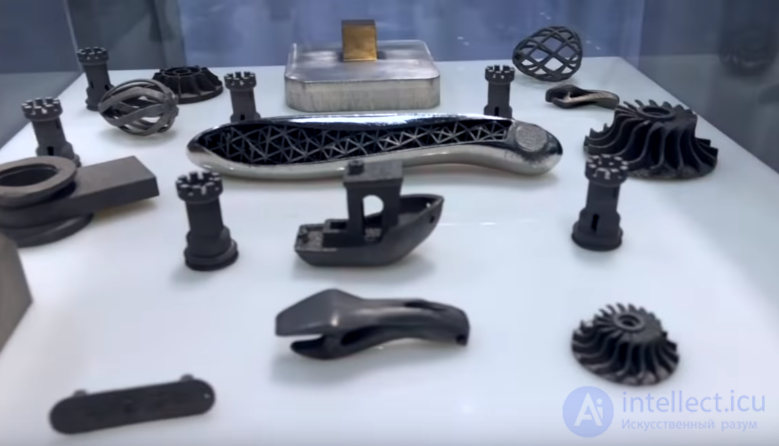
metal items printed on 3D printers
Direct metal laser sintering (DMLS) is an additive manufacturing technology for metal parts developed by the Munich-based company EOS. DMLS is often confused with the similar technologies of selective laser sintering ("Selective Laser Sintering", or SLS) and selective laser melting ("Selective Laser Melting", or SLM). Powdered material is fed into the build chamber in the amount needed to deposit a single layer. A special roller levels the delivered material into an even layer and removes the excess material from the chamber, after which the laser head sinters the particles of fresh powder to one another and to the previous layer along the contours defined by the digital model. Once the layer has been traced, the process repeats: the roller delivers fresh material and the laser begins to sinter the next layer. Another interesting feature of the process is that there is no need to build supports for overhanging elements of the design. The unsintered powder is not removed during printing but remains in the build chamber. Every subsequent layer therefore has a supporting surface. In addition, the unused material can be collected from the build chamber once printing is complete and used again. DMLS production can be considered practically waste-free, which is important when expensive materials – precious metals, for example – are used.
+ the ability to rapidly produce geometrically complex parts without machining (the so-called "subtractive" methods – milling, drilling and so on).
+ Production is practically waste-free.
+ several models can be built at the same time, limited only by the size of the build chamber
+ building models takes on the order of a few hours, which is incomparably more advantageous than casting, which can take up to several months when the full production cycle is counted.
disadvantages -
- parts produced by laser sintering are not fully solid, and therefore do not reach the same strength figures as cast samples or parts made by subtractive methods.
Electron beam melting ("Electron Beam Melting", or EBM) is a method of additive manufacturing of metal parts. This technology is often classified as a rapid manufacturing method. Electron beam melting (EBM) is similar to selective laser melting (SLM) – the main difference lies in the use of electron emitters (so-called electron guns) instead of lasers as the energy source for melting. The technology is based on the use of high-power electron beams to fuse metal powder in a vacuum chamber, forming successive layers that follow the contours of the digital model. Unlike sintering technologies, electron beam melting makes it possible to create parts of especially high density and strength.
This method of producing parts of arbitrary shape makes it possible to create high-density metal models from metal powder.
The consumables consist of pure metal powder with no binder filler, and the finished models are not porous. As a result, the printed model does not have to be fired to achieve the required mechanical strength. This aspect places EBM alongside selective laser melting (SLM) and apart from selective laser sintering (SLS) and direct metal laser sintering (DMLS), which often require firing after printing to reach maximum strength characteristics. Compared with SLS, SLM and DMLS, EBM offers a higher build speed thanks to the greater power of its emitters and to electronic rather than electromechanical deflection of the beams.
Electron beam melting is carried out at elevated background temperatures of around 700-1000°C, which makes it possible to create parts that do not suffer from the residual mechanical stress caused by the temperature gradient between already cooled and still hot layers. In addition, completely melting the consumable powder yields fully solid items – hence the maximum strength and the absence of any need for firing.
The technology was developed and first used by the Swedish company Arcam AB.
Applications

A craniofacial implant made using EBM technology
Using titanium alloys as consumables allows EBM technology to be applied to the production of medical implants.
Since 2007, two European companies, Adler Ortho and Lima Corporate, together with the American company Exactech, have used EBM technology to manufacture acetabular cups (hip joint implants).
The technology has found application in the aerospace industry: Boeing, Lockheed Martin and NASA use EBM to produce parts for jet and rocket engines as well as load-bearing structural elements of aircraft.
The 3DP method consists of depositing glue onto the material, then a layer of fresh powder on top of it, and so on over and over. The result is a material resembling gypsum (sandstone). If pigment is added to the glue, colored objects can be produced. The technology is safe for home and office use. Suitable materials include glass, bone, rubber and even wood-sawdust powders. Edible figurines can also be made (using chocolate or sugar powders) – only in that case a special food-grade glue is used.
There are drawbacks as well – the final result may have a rough surface and low resolution.
Gcode is a text file in a simple format - a set of commands, one per line, that the control electronics of our 3D printer understand. The same format is used for CNC machines.
For example, the lines
M106 ; fan on
G28 ; home all axes
G1 Z5 F5000 ; lift nozzle
mean the commands to switch on the fan on the extruder, then move the extruder to the home coordinates on all axes, and then raise the nozzle. These are usually followed by the commands that actually print your part.
The rapid development of additive printing technologies would have been impossible without modern software. In the past, you had to spend a long time mastering graphics editors and learning the basics of engineering modeling in order to create even the simplest objects.
Today's 3D printer software makes it possible to automate the printing process almost completely and to greatly simplify the handling of this high-tech equipment.
Virtually all 3D printing devices are controlled by so-called G-code – the generally accepted language used for machines of this kind.
This is the name given in the 1960s to the language for CNC machine tools. It was first developed by the American Electronic Industries Alliance, and was then adopted by virtually all manufacturers and users of automated machine tools.
G-code defines the structure and syntax for writing commands for a machine tool. G-code has an international basic structural foundation approved by the American and European standardization systems. However, there are many specific extensions and modifications used locally by machine tool manufacturers and by large corporations that produce equipment.
To obtain any part in 3D, two problems must be solved:
Special 3D printer programs exist both for building three-dimensional objects and for controlling printing.
Programs that perform 3D printing work with models of three-dimensional objects. Not only do they use different file structures, they also differ in their content. Models of three-dimensional objects fall into two types:
A solid object (Solid) is a vector model that describes the body completely by means of mathematical vectors. In it, every point has values (coordinates, weight, color, any other properties). Because the properties and coordinates are described by vectors, such an object has infinite detail.
A surface object (Mesh) is a model described by a "mesh". Only the "threads" of the mesh that wrap around the object's surfaces are described by mathematical vectors. The mesh has a spacing between threads that determines the accuracy with which the properties of the model and its parts are described.
Solid models contain a great deal of information, which demands a large amount of resources. Surface objects are considerably smaller in size, but the accuracy with which their properties are represented is limited by the mesh parameters.
Some industrial printing devices, like sophisticated CNC machine tools, "know how" to work with solid data sets. However, all mass-market consumer and industrial printers are designed to work only with surface (mesh) models.
A slicer was originally a utility able to cut a surface data set into parallel planes and convert the resulting information into G-code. After all, extruder heads work in exactly this way, building an object by successively adding "slices" of surfaces in parallel planes.
That is why, when three-dimensional printers entered the market, utilities appeared that slice these planes and then drive the stepper motor drivers and the printer's nozzles. As printing in this field developed, slicers also began to be equipped with simple tools for building three-dimensional objects.
Tools originally intended for three-dimensional modeling are far more powerful. They can be used to build objects of any complexity and level of detail. But working with them requires certain skills. Nevertheless, CAD tools (CAD or CADD — computer-aided design system) have also advanced considerably with the advent of three-dimensional printing. Today all powerful modeling programs have built-in capabilities for compiling their models into a *.stl file.
The development of printing with solid materials is proceeding along several paths. Developers of slicers and of other useful application software are not standing still either. For example, attempts have appeared to present the finished part with all its possible flaws and limitations. This can be very useful. Powerful CAD systems cannot yet boast such useful capabilities, although their applications implement similar things for casting and machining.
In addition, slicer interfaces are made intuitive and very simple for the user. Simple objects are much easier to build in a slicer, even for an experienced CAD user. A major advantage of slicers, besides simplicity and accessibility, is the cost factor. Most of them are free and freely distributable. There are paid tools as well, but their cost is not that high compared with the cost of CAD. All good slicers and front ends have tools for editing and building simple objects.
If you already use a 3D printer, a slicer program came with it, along with initial settings. However, this is not always enough to solve your tasks. Software for a 3D printer is still supplied by the manufacturer without regard to individual user needs.
The programs used for working with a 3D printer are mostly free. Only some of them have paid versions or extensions. All the free programs provided for 3D printers by developers are still supported and updated free of charge as well. Many of them are open source.
Software distributed for 3D printers with a Russian-language interface is still fairly scarce. But the domestic market is growing quite quickly, and the amount of localized software is increasing. The order of the utilities presented below is based on their worldwide popularity.
The most widespread slicers and other useful software for 3D printers are presented below:
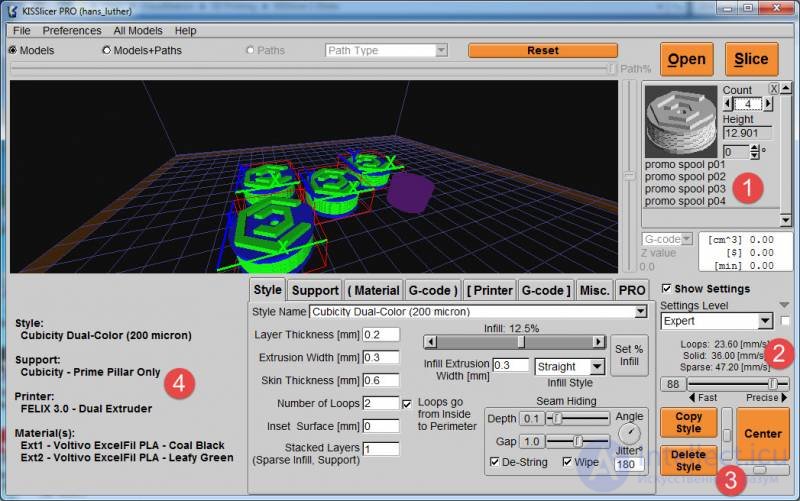
One of the most popular tools for working with model printing. There are paid and free versions. The paid one differs in its support for multiple nozzles, a cloud service, libraries, and a larger number of settings and tools.
Almost all the paid options are needed for machines with several nozzles and for building complex objects. It does not offer extensive editing capabilities. On the other hand, it implements direct G-code editing, which makes it possible to control all of the machine's components directly.
The free version is available for any operating system. On the same page you can move on to the paid professional version.
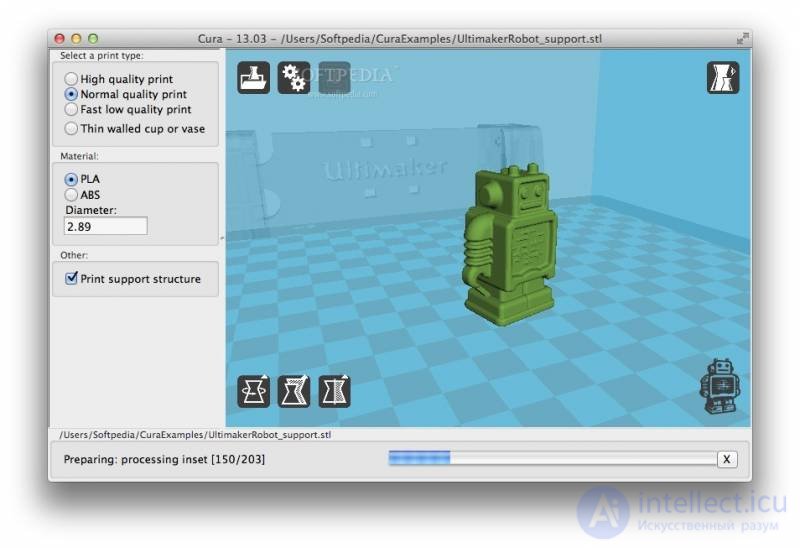
One of the most convenient and intuitive applications, from 3D printer manufacturer Ultimaker. It has become the most widely used – it is the most popular slicer for 3D printers. Besides editing tools, material settings and print options, it includes a number of handy functions for calculating the amount of material and its cost, and the weight of the part. It is open source. A completely free, regularly updated utility.
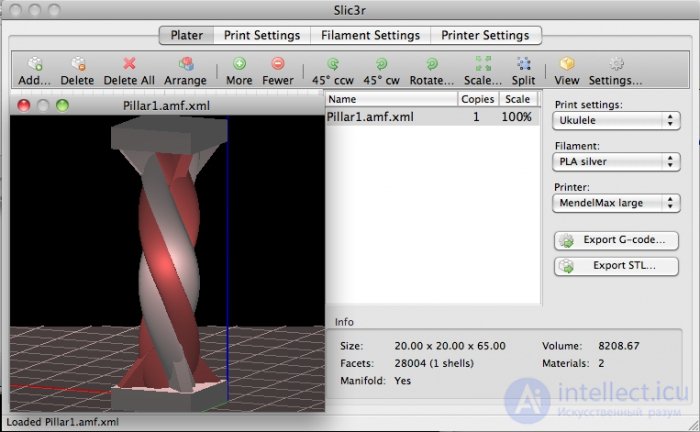
One of the most versatile and well-developed products in terms of building and editing G-code for a printer. It has settings for virtually all printing functions themselves, support for several nozzles and for several types of material in use. Editing of G-code by the user is implemented.
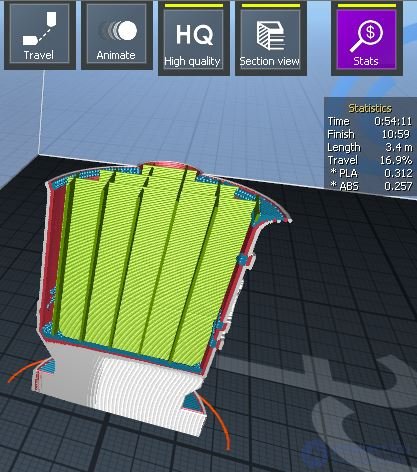
This utility is built very intuitively and simply. At the same time, it has several advantages. Three modes divide the preparation for creating a part into separate functions:
Print settings are implemented separately. There are functions for determining the time and the estimated cost, and a function for viewing the build phases over time.
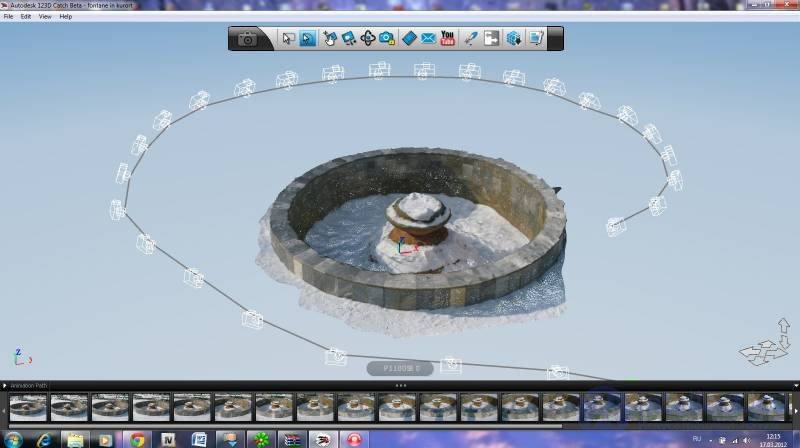
This is a tool from Autodesk that lets you create a 3D object from camera shots. There is also an Android version that turns a smartphone into a 3D scanner. Processing shots taken from various angles produces a three-dimensional surface object in several common 3D graphics formats.
All operations are carried out in a cloud service, with email used to receive the final file. The part is visualized directly within the utility. It is distributed and supported free of charge.
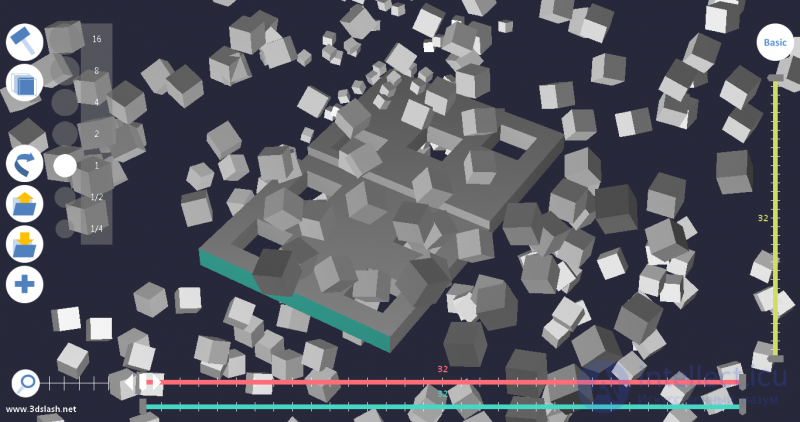
A very powerful cloud-based program that lets you create, edit and print 3D objects. Its intuitive, interactive interface makes all of its functions easy to grasp and use. Besides loading, creating and editing objects, it implements all the functions of a slicer and of print control. It is perhaps the simplest and most versatile program for a 3D printer, allowing you to create and print all kinds of objects.
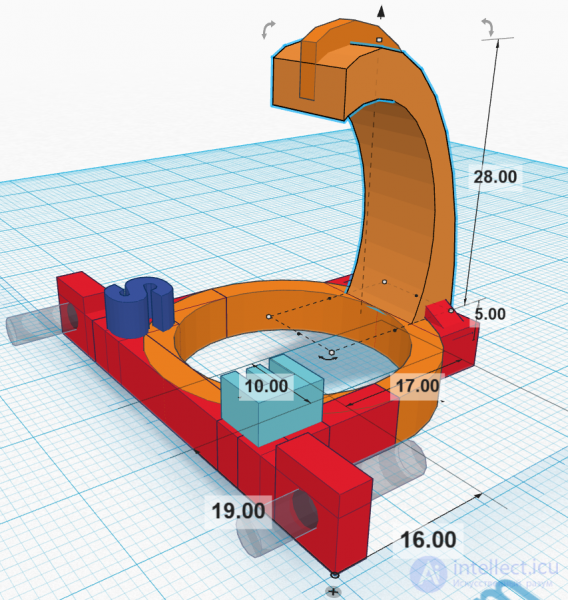
A fully cloud-based service from Autodesk that lets you work with 3D models, create them, edit them and send them to print. It offers a very large number of services and capabilities, and functions for building and for controlling printing. It is not the most functional utility for controlling a printer, since it was originally developed for other kinds of application machines, but these functions are being continuously developed by the vendor and their coverage of various standards is increasing.
You can start using the service with a Russian-language interface after registering at https://www.tinkercad.com/ . A short training course is also offered there.
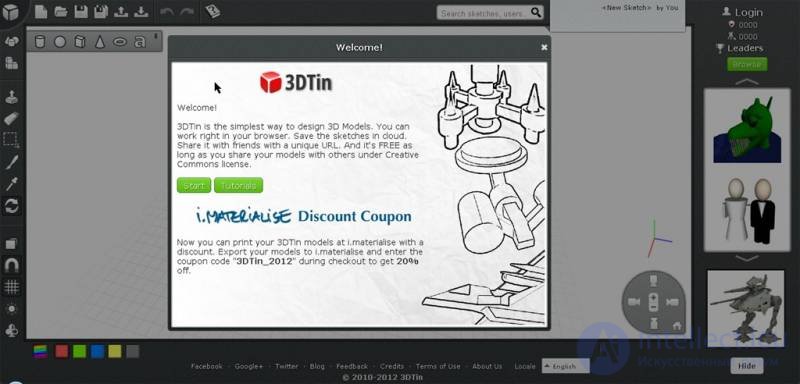
An online editor for building and editing mesh 3D models. Very simple, fast and intuitive. It requires no prior skills. It works only in the cloud. It allows simple objects to be created and then converted into stl files.
The service is one of the freely distributed CAD tools, which can only be used after registering at https://www.tinkercad.com/ or at Autodesk's tool server http://formit360.autodesk.com/.
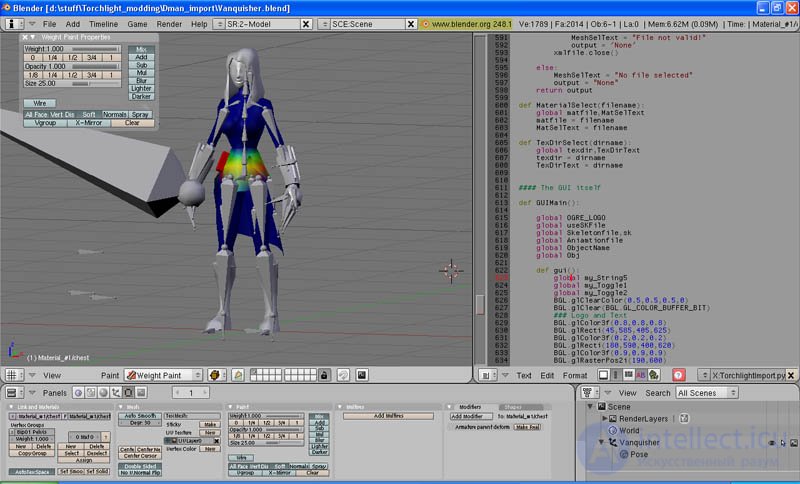
An interesting three-dimensional editor. Very simple, yet quite functional for building various parts from a large library of primitives. There is a set of convenient tools for editing. It saves files in most of the formats in use, so it is often used as a converter. The utility was originally written for three-dimensional animation, but continuous refinements and extensions have made it perfectly suitable for designing parts. The tool is distributed free of charge and is open source.
3D printing attracts a great many people who take an interest in it out of personal curiosity or for production purposes. For those with no experience at all in this field, learning the art of three-dimensional printing, whether in online or in-person courses, will not be difficult. Something else matters more: exactly what purposes such a machine is being bought for. Setting priorities correctly, combined with knowledge of the technology used for a given area of application, will allow the equipment to be used to its full potential.
The list of three-dimensional printing tools presented here is far from complete – many more already exist. New ones appear, and existing ones improve very quickly. Intuitive G-code editing capabilities, simple ways of editing surface objects, and tools for visually controlling the actual printing functions are appearing. We are on the threshold of a technological take-off in this new industry, making our own modest contribution as users to its establishment and improvement.

Comments